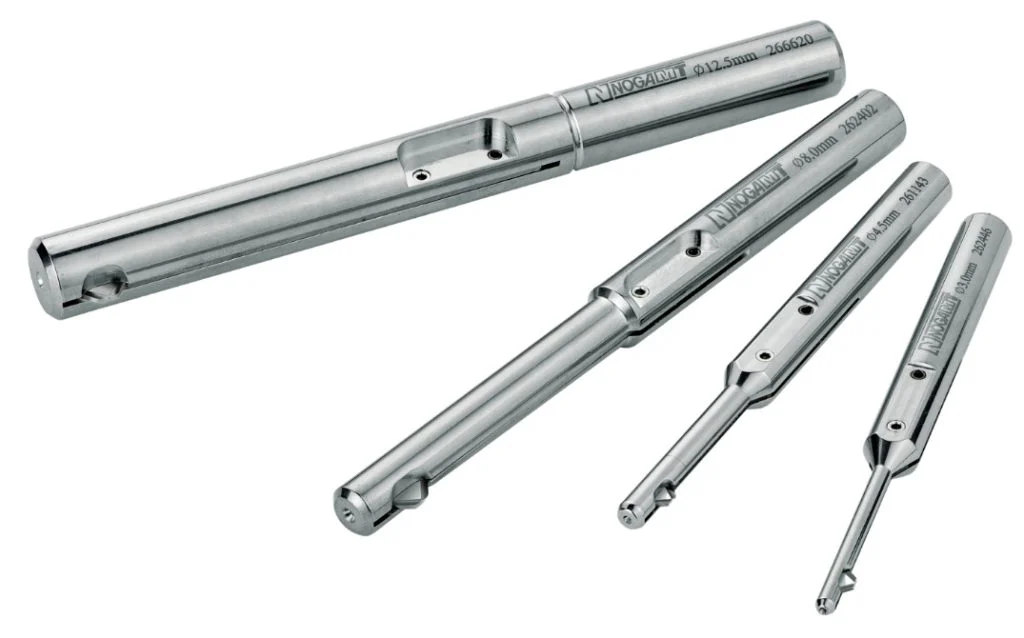
Front and back hole deburring in one pass. Select material and blade configuration, then match the holder by pilot hole or by thread and validate inclined / tube geometry. All data is the NOGA MT UBURR Technical Center source data and works offline.
Metric (mm) Inch (in)
Standard pilot range Ø2.5–<Ø25.5mm (0.098–<1.004 in) 1.Material & blade 2.Tool / thread & machine values 3.Inclined & tube
Search material / condition / AISI / DIN Blade configuration HSS uncoated HSS coated Carbide coated
All P M K N S H C
43of43source conditions
P·Annealed Non-alloy steel and cast steel, free cutting steel <0.25% C · AISI 1020 · DIN 1.0044 P·Annealed Non-alloy steel and cast steel, free cutting steel ≥0.25% C · AISI 1035 · DIN 1.0501 P·Quenched and tempered Non-alloy steel and cast steel, free cutting steel <0.55% C · AISI 1045 · DIN 1.1201 P·Annealed Non-alloy steel and cast steel, free cutting steel ≥0.55% C · AISI 1055 · DIN 1.0535 P·Quenched and tempered Non-alloy steel and cast steel, free cutting steel ≥0.55% C · AISI 1060 · DIN 1.1221 P·Annealed Low alloy and cast steel (less than 5% of alloying elements) AISI G92600 · DIN 1.5028 P·Quenched and tempered Low alloy and cast steel (less than 5% of alloying elements) AISI 4130 · DIN 1.7218 P·Quenched and tempered Low alloy and cast steel (less than 5% of alloying elements) AISI 4142 · DIN 1.2332 P·Quenched and tempered Low alloy and cast steel (less than 5% of alloying elements) AISI 5045 · DIN 1.7006 P·Annealed High alloyed steel, cast steel and tool steel AISI H13 · DIN 1.2344 P·Quenched and tempered High alloyed steel, cast steel and tool steel AISI M33 · DIN 1.3249 P·Ferritic/martensitic Stainless steel and cast steel AISI 420 · DIN 1.4021 P·Martensitic Stainless steel and cast steel AISI 420 · DIN 1.4021 M·Austenitic, duplex Stainless steel AISI 304L · DIN 1.4306 K·Ferritic / pearlitic Gray cast iron (GG) AISI Class 25 · DIN 0.6015 K·Pearlitic / martensitic Gray cast iron (GG) AISI Grade H20 · DIN 036037 K·Ferritic Nodular cast iron (GGG) AISI 60-40-18 · DIN 0.7043 K·Pearlitic Nodular cast iron (GGG) AISI F33500 · DIN 0.7050 K·Ferritic Malleable cast iron AISI A47 · DIN 0.8135 K·Pearlitic Malleable cast iron AISI A220 Class · DIN 0.8155 N·Not hardenable Aluminum-wrought alloys AISI 5005 · DIN 3.3315 N·Hardenable Aluminum-wrought alloys AISI 7075 · DIN 3.4365 N·Not hardenable Aluminum-cast alloys ≤12% Si · AISI 518.0 · DIN 3.3292 N·Hardenable Aluminum-cast alloys ≤12% Si · AISI 515.0 · DIN 3.3241 N·High temperature Aluminum-cast alloys >12% Si · AISI 390 · DIN N·Free cutting Copper alloys >1% Pb · AISI C36000 · DIN 2.0375 N·Brass Copper alloys AISI C22000 · DIN 2.0230 N·Electrolytic copper Copper alloys AISI C63000 · DIN 2.0966 N·Duroplastics, fiber plastics Non metallic AISI Bakelite · DIN N·Hard rubber Non metallic AISI Ebonite · DIN S·Annealed High temperature alloys Fe based · AISI 330 · DIN 1.4864 S·Hardened High temperature alloys Fe based · AISI S590 · DIN 1.4977 S·Annealed High temperature alloys Ni or Co based · AISI Incoloy 825 · DIN 2.4858 S·Hardened High temperature alloys Ni or Co based · AISI Inconel 718 · DIN 2.4668 S·Cast High temperature alloys Ni or Co based · AISI Nimocast K24 · DIN 2.4674 S·Pure Titanium alloys AISI Titanium G.1 · DIN 3.7024 S·Alpha+beta alloys, hardened Titanium alloys AISI Titanium G.5 · DIN 3.7165 H·Hardened Hardened steel AISI HARDOX 500 · DIN H·Hardened Hardened steel AISI HARDOX Extreme · DIN H·Cast Chilled cast iron AISI A532 lllA 25% Cr · DIN 0.9650 H·Hardened Cast iron AISI A532 IID 20% CrMo · DIN 0.9645 C·Cured Carbon Fiber reinforced plastics (CFRP) C·Cured Glass Fiber reinforced plastics (GFRP) Setup stability (affects feed only) Stable (× 1.0 feed) Moderate (× 0.9 feed) Poor (× 0.7 feed)
Source cutting data
Material Non-alloy steel and cast steel, free cutting steel · <0.25% C
Condition Annealed
AISI / DIN 1020 / 1.0044
Blade configuration HSS coated
Cutting speed Vc (source) 45-65 m/min · 100-165 sfm
Feed per revolution (source) 0.08-0.20 mm/rev · 0.003-0.008 ipr
Feed after stability (Stable × 1) 0.08–0.2 mm/rev
Chip former ML / PL
Coolant Air / Wet Source cutting speed is never modified by stability — only feed is.
All calculated values are starting recommendations based on NOGA MT source data. Validate on the actual application, machine and fixture.